Welcome to our websites!
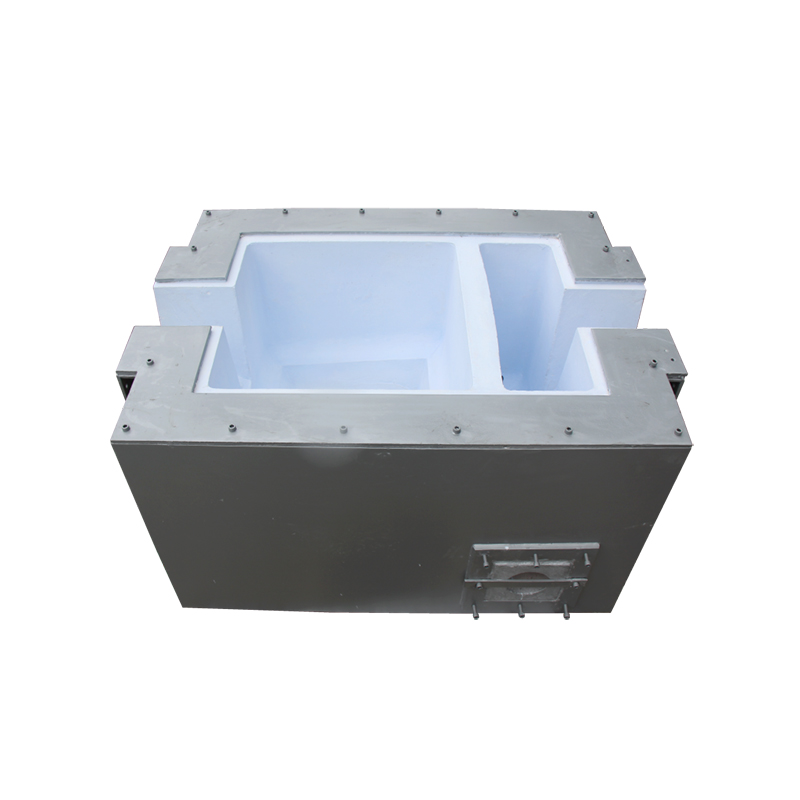
Factory wholesale Tc Casting - filter box with ceramic filter board filtering molten aluminum – ZheLu
Factory wholesale Tc Casting - filter box with ceramic filter board filtering molten aluminum – ZheLu Detail:
1. It can be used directly at room temperature without worrying about thermal shock.
2. No thermal expansion and low thermal conductivity.
3. It can float in aluminum, reducing the possibility of refractory inclusions.
Product detail pictures:
Related Product Guide:
Our products are mainly used in the smelting process of the aluminum casting industry and the extrusion process of aluminum profiles. Factory wholesale Tc Casting - filter box with ceramic filter board filtering molten aluminum – ZheLu , The product will supply to all over the world, such as: Guatemala, Jordan, Czech republic, Aluminum extrusion molding (or aluminum extrusion) is a plastic working method that applies strong pressure to the aluminum billet placed in the mold cavity (or extrusion cylinder), forcing the aluminum billet to produce directional plastic deformation and extrude from the die hole of the extrusion mold, so as to obtain the required cross-sectional shape, size and certain mechanical properties of the parts or semi-finished products.
 By Christian from Malta - 2018.12.25 12:43
This company conforms to the market requirement and joins in the market competition by its high quality product, this is an enterprise that have Chinese spirit.
By Victor Yanushkevich from Canada - 2018.11.06 10:04
Products categories
-
Good User Reputation for Hydraulic Oil Cooling ...
-
Competitive Price for Die Heating Furnace - Dr...
-
factory customized Precision Refractory Service...
-
Excellent quality Aluminium Profile Stand - Va...
-
Online Exporter Casting Molten Aluminum - 600-...
-
Hot-selling Electric Heating Tube - High densi...