factory low price Casting Plate - High quality Adc12 99.7 A7 A Grade Aluminum alloy Ingots – ZheLu
factory low price Casting Plate - High quality Adc12 99.7 A7 A Grade Aluminum alloy Ingots – ZheLu Detail:
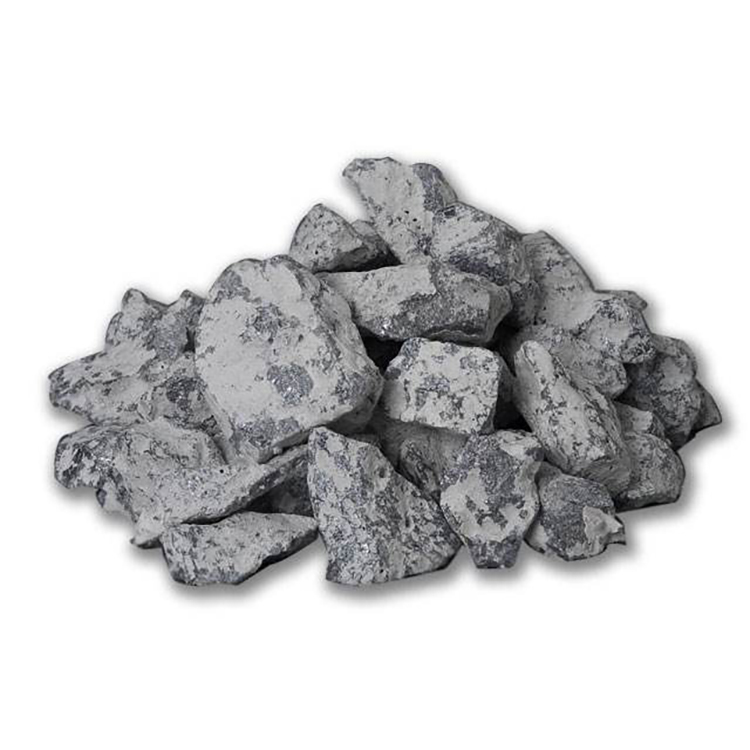
After all the charge is melted, stir well and take samples for analysis. Calculate the addition amount of fast-melting silicon according to the analysis results. When the molten aluminum reaches 740-770 °C (the process of adding silicon is an endothermic reaction, the temperature of the molten metal must be heated to keep the temperature not lower than 740 °C), throw the instant silicon agent on the molten aluminum surface for use, and press the bell into the molten aluminum. Stir in for 2-5 minutes. Product description: The silicon content is 95%, and it can be rapidly melted at low temperature, which greatly reduces the cost of alloy ingredients, and can quickly prepare any silicon-aluminum alloy with silicon content; the composition control is extremely precise, and a large number of inclusions and harmful substances that are easily brought into the master alloy are eliminated. Impurities, to avoid the use of waste miscellaneous aluminum to prepare aluminum-silicon master alloys and the impact on the quality of the final aluminum alloy that is difficult to control.
Product detail pictures:
Related Product Guide:
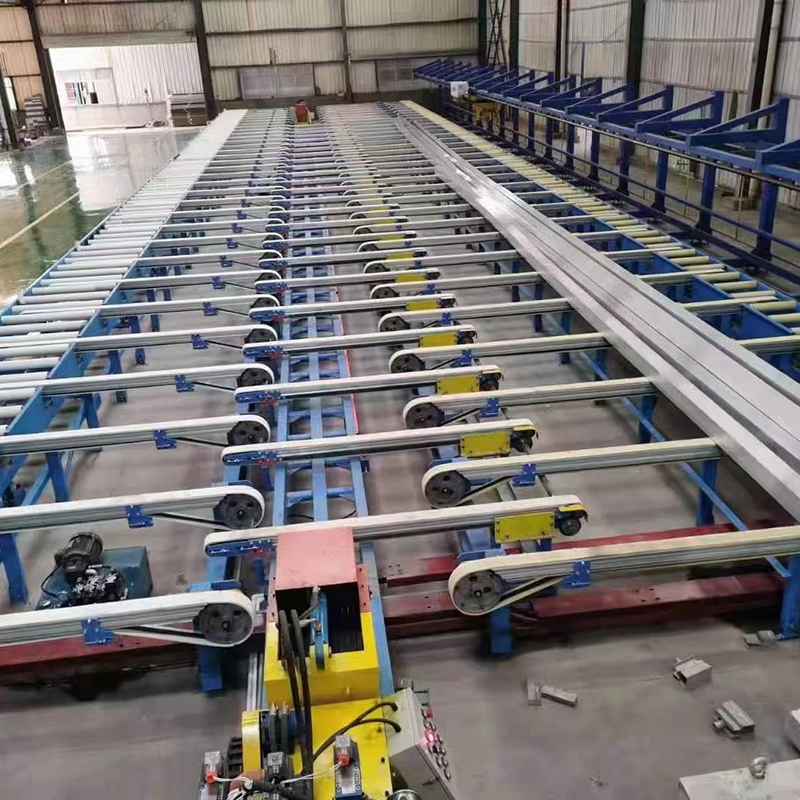
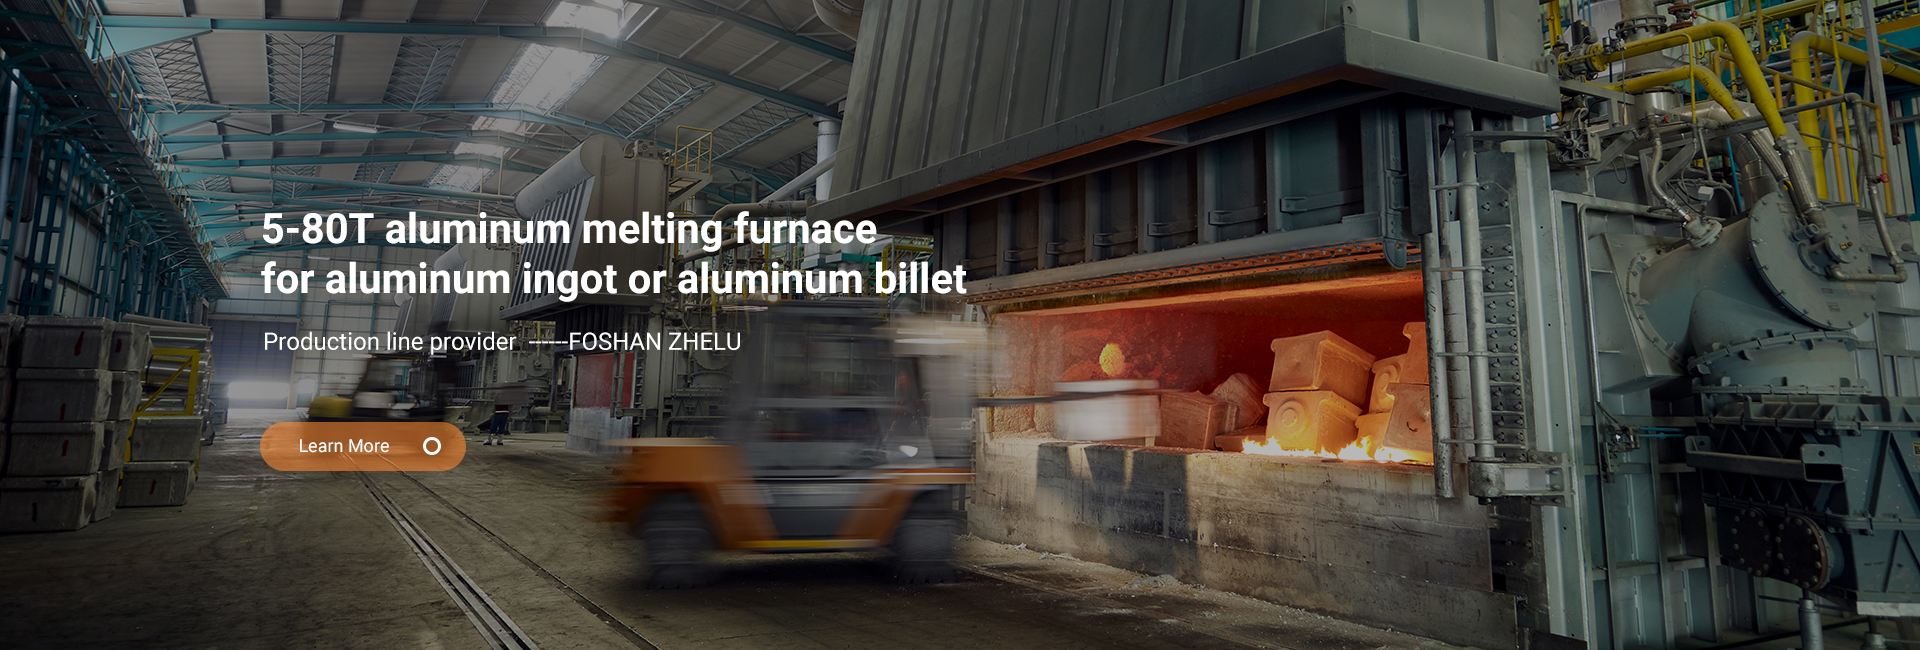
We have a minimum capacity of 500KG medium frequency furnace, electric furnace, etc. for aluminum plants with small output, and there are also fixed large-scale aluminum melting roads with a capacity of 5UST to 88UST, for aluminum casting plants with larger output. factory low price Casting Plate - High quality Adc12 99.7 A7 A Grade Aluminum alloy Ingots – ZheLu , The product will supply to all over the world, such as: Belize, Malta, America, Under the action of pressure, the heated aluminum rod is divided into several metal flows, enters the welding chamber through the shunt hole, collects in the welding chamber, and is welded again in the environment of high temperature, high pressure and high vacuum, and finally flows out through the gap between the mold core and the die hole, so as to form a pipe or hollow aluminum profile that meets the size and performance requirements, as an aluminum door and window profile or industrial aluminum profile. If bending is required, a bending tool is added to the rear device.
 By Riva from
Melbourne -
2017.04.18 16:45
In general, we are satisfied with all aspects, cheap, high-quality, fast delivery and good procuct style, we will have follow-up cooperation!
By Monica from
Dubai -
2017.06.29 18:55